Hey everyone, it’s Jake from the team that sells automatic hot press welding machines—you know, the ones that take all the hassle out of welding thick materials without requiring 10 years of welding experience. I get it, when you first take one of these bad boys out of the box, it can feel like you’re staring at a alien spaceship. No shame there—we’ve all been overwhelmed by fancy industrial gear that looks like it’s built for rocket scientists. But today, I’m walking you through the whole install process, step by step, like I’m ranting to a buddy over coffee (minus the actual coffee spills, promise). This is the same process we use when we drop off a machine at a client’s shop, and it works every single time. No shortcuts, no confusing jargon, just real, doable stuff. Fully Automatic Hot Press Welding Machine
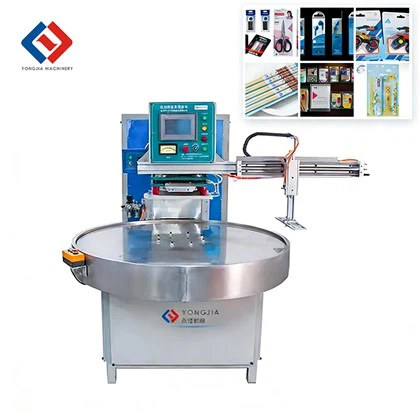
First things first, you can’t just unbox it and plug it in, okay? That’s how you fry the control panel, or worse, hurt yourself. Let’s start with the prep work—most people skip this part and end up calling me at 7 PM panicking because they don’t have the right space. What do you need here? Well, first, the machine itself isn’t tiny. Our standard fully automatic hot press is about 8 feet long, 6 feet wide, and weighs over 2,000 lbs. So you need a spot that’s flat, level, and has enough room around it for you to move materials, access the doors, and run the cable. I’m talking like 3 extra feet on all sides, minimum. No shoving it into a corner where you can’t reach the emergency stop button— that’s non-negotiable.
Also, power. Don’t just look at your wall outlet and think “that’ll work.” These things pull a lot of juice—usually 3-phase 480V, some of the bigger models even need 600V, and you can’t just convert a regular 120V outlet. You need a licensed electrician to come check your panel and run the correct line before the machine even shows up. I’ve had clients try to wing this, and they ended up blowing a breaker in the whole shop when they powered on the press. Save yourself the headache—pay the electrician $200 now instead of $1,500 in repairs later.
Next, the machine delivery and offloading. Yeah, I know this part sucks, but if you’re getting it shipped, it’ll come on a skid, and you need a forklift or a pallet jack that can handle at least 2,500 lbs (just to be safe—extra weight for the skid). Don’t try to hoist it with a regular dolly, that’s how you drop a $50k machine and break the hydraulic arm. Once it’s in the spot, you need to level it. Most shops have concrete floors, but they’re never perfectly flat. Grab a level, stick it on the top of the press table, and adjust the adjustable feet (we put four big ones on every machine for this exact reason) until it’s dead level—like, within 1/8 of an inch across the whole table. If it’s not level, the welds will be uneven, and you’ll get garbage results. Trust me, I’ve seen it go wrong when a client skipped this step, and they had to redo 100 parts.
Okay, now the physical connections. This is where the fun starts, no more prep. First, the hydraulic lines. On the side of the machine, there are two big metal tubes—don’t mix them up, they’re labeled “in” and “out” for hydraulic fluid. The good news is we use quick-connect fittings, so you just line them up, push till they click, and they’re sealed. No wrenches needed here, which is nice because you don’t want to strip the threads and cause a leak. Wait, but before you connect the power, double check all the fittings are tight? Yeah, maybe, just in case.
Then the power cable. Again, this is where the electrician comes in. We send a pre-terminated power cable with every machine, so all you have to do is run it from the breaker you had installed back to the press, then plug it into the main power port on the back (it’s a big, heavy-duty plug, not your regular laptop charger). Once that’s in, turn the breaker on, but don’t hit the power button on the machine yet. We need to prime the hydraulics first. That’s a super simple step: there’s a little manual bleed valve on the hydraulic pump. Open it, turn the pump on (there’s a small switch on the control panel for that), and let it run for 30 seconds to a minute, until no more air comes out of the valve. Then close it tight—if air gets in the lines, the press will be slow and unresponsive, which is a nightmare for consistent welds.
Wait, if you’re wondering why we don’t prime it before shipping—because air can get in during transport, so it’s something you need to do on-site. That’s not just us being extra, that’s how all good industrial gear works.
Now the control panel setup. This is the part that trips people up, but it’s actually way easier than it looks. The control panel has a touchscreen, right? You’ll get a little USB drive with the default settings for your machine size—just plug that into the USB port on the panel, and it’ll load the presets. These presets are for different materials: steel, aluminum, copper, even some specialty alloys. You don’t have to mess with the temperature, pressure, or weld time right away, unless you’re working with something super specific that’s not in the default list.
Quick tip: change the admin password right away. The default is usually “1234” and every tech who’s ever worked on a machine knows that. I’ve had clients come to me a month after install saying someone messed up their settings, and it’s because they left the default password. Take 2 minutes to make a new one. Also, turn on the automatic save feature in the settings—if the power cuts out, it won’t wipe all your custom presets. That’s a lifesaver, trust me.
Next, the tooling setup. Wait, tooling is the stuff that actually touches the parts you’re welding—like the die and the electrode heads. Every machine comes with standard tooling, but if you’re working with custom parts, you’ll have to swap them out. That’s easy too: there are four bolts holding each electrode head on, just loosen them with an Allen wrench, slide the old one off, and slide the new one on, then tighten the bolts back up. Make sure the heads are aligned—they should sit perfectly parallel on the press table, not tilted, otherwise your weld will be off-center. Once they’re on, run a test weld on a scrap piece of your material first, just to make sure the alignment is right. No need to waste good parts yet.
Speaking of test welds, that’s the next step. Before you run a full production run, do at least 3 test welds on scrap material. Why? Because even if you followed every step, sometimes the pressure is a little off, or the temperature is too high/low. Let me tell you a story: a client of mine last year thought he was done after loading the presets, ran the first part, and it was garbage. Turns out the scrap steel he used for testing was thicker than his actual production parts, so the pressure was set too high. Do test welds, and check them with a angle grinder or a pressure tester—make sure the weld holds up, no gaps, no burn-through.
Also, there are a few safety checks you can’t skip. This is non-negotiable, because these machines can crush stuff (or fingers) if you’re not careful. First, test the emergency stop button. It’s the big red one on the control panel—hit it, and the press should stop moving immediately, no delay. If it doesn’t, don’t use the machine, call me right away. Second, check the safety guards. The press has little metal covers that block you from putting your hand in while it’s moving. Don’t remove these guards—no matter how much of a rush you’re in. I know some welders hate working around guards, but they’re there for a reason. Third, make sure the floor around the machine is clear of clutter, oil, or tools. No one wants to slip and fall while the press is moving.
Wait, what about if you have a smaller model, like the tabletop ones? I get it, some of you are startups or small shops that don’t have a ton of space. The process is almost the same, just lighter. You don’t need a forklift to offload them, you can move them with a hand truck, and they run on standard 240V power, not 3-phase. But even the tabletop ones need to be level, and you still need to do the test welds and safety checks. Don’t try to cut corners just because it’s smaller.
Okay, now once you’ve done all that, you’re ready to go! But wait, I always tell new owners to spend the first week getting familiar with the control panel. Don’t jump into production. Spend time messing with the settings, watching how the press moves, doing more test welds. Every material is a little different, so even if the preset says it’s good, you might need to tweak the weld time by 0.5 seconds or the pressure by 10 PSI. That’s normal.
Now, let’s talk about common mistakes I see people make during install, because I’ve heard them all. First, not level the machine. Like I said earlier, that’s a big one—uneven levels = bad welds. Second, mixing up the hydraulic lines. If you hook the “in” line to the “out” port, you’ll blow a seal, and that’s a $300 repair part. Third, skipping the prime step for the hydraulics. Air in the lines makes the press act weird, and you’ll waste so much time troubleshooting when it’s just air. Fourth, not testing the emergency stop. I had a client who hit the E-stop once and it didn’t work, and he told me he would’ve lost a hand if he wasn’t paying attention. Don’t be that guy.
Oh, and if you run into a problem during install? Don’t Google random YouTube videos that were made for a different brand of machine. Our team has free support for the first 90 days after install, and we’re on call 24/7 for urgent stuff. Just send us a message or give us a call, we’ll walk you through it. No need to stress over a tiny issue that could be fixed in 2 minutes.
Before I wrap this up, let’s do a quick recap, so you don’t forget anything: 1) Prep your space (flat, level, enough room, correct power) and get a licensed electrician first. 2) Offload and level the machine with adjustable feet. 3) Connect hydraulic lines (don’t mix in and out), power, prime hydraulics. 4) Load default presets, change password, turn on auto save. 5) Set up tooling, align electrodes. 6) Do test welds, check safety features. 7) Familiarize yourself with the machine before full production.

If you’re in the market for a fully automatic hot press welding machine, we’ve got models for every size shop—from small tabletop ones for startups to big industrial ones for large fabrication facilities. Whether you’re welding steel, aluminum, copper, or specialty alloys, we’ll set you up with the right machine, and our team will walk you through every step of install just like I did here. No pushy sales stuff, just honest advice and a machine that works as hard as you do.
Fully Automatic Production Line If you have any questions about install, models, or anything else, don’t hesitate to reach out. We’re here to help you get your shop running smoothly.
References
- Industrial Press Installation and Safety Standards. National Institute of Occupational Safety and Health, 2022.
- Fully Automatic Hot Press Welding Machine Operational Manual. Precision Welding Equipment Co., 2023.
- Small Business Industrial Machinery Setup Best Practices. Small Business Administration, 2021.
Dongguan Yongjia Machinery Equipment Co., Ltd.
We are one of the most reliable fully automatic hot press welding machine manufacturers and suppliers in China, specialized in providing high quality customized service. Please feel free to wholesale advanced fully automatic hot press welding machine at low price from our factory. For quotation, contact us now.
Address: No. 240, Chashan South Road, Chashan Town, Dongguan City, Guangdong Province, China
E-mail: info@yjwelding.com
WebSite: https://www.yjhighfrequencymachine.com/
