If you’re here, you’re probably either a bore welder gearing up for your next big job, a workshop manager figuring out what’s missing from your tool cart, or maybe someone who’s just heard of bore welding and wants to know why it’s not just sticking a rod in a machine and calling it a day. Let me tell you straight: I’ve been supplying bore welding gear for what feels like a lifetime (no, I won’t say “decades” because that sounds stiff—let’s just say I’ve seen more botched bore welds than I care to admit), and the #1 mistake I see new guys make is skipping on the right accessories. It’s not just about the main welder itself—those little add-ons make or break a job, keep you safe, and save you from rework that’ll cost you way more than the parts you skipped buying. Bore Welder
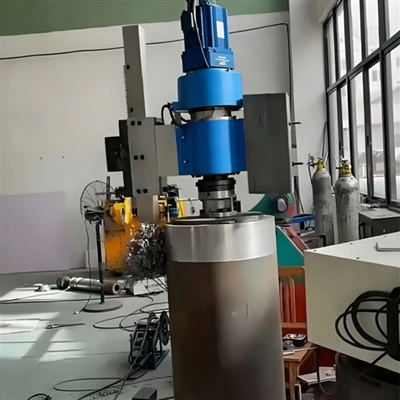
First off, let’s talk about the boring stuff you can’t skip because it’s non-negotiable for quality. I’m talking about back-up rings. Wait, don’t roll your eyes—back-up rings sound simple, but trust me, they’re make-or-break. When you’re welding a bore, especially on big stuff like hydraulic cylinders or excavator booms, the weld pool wants to drop into the gap if you don’t have something holding it up. Cheaper rings are flimsy, warp after one job, and leave a messy, weak weld. The good ones? They’re made of precision-machined carbon steel, fit the exact inner diameter of your bore, and some even have a ceramic coating so they don’t stick to the weld metal. I once had a guy bring in a cylinder he messed up because he used a old washer as a back-up—turns out, the washer melted in half mid-weld and he had to scrap the whole cylinder. Don’t be that guy.
Next, preheat torches. Wait, why? Bore welding is all about thick steel, right? Excavator booms, engine blocks, pump housings—those are all heavy, high-carbon or alloy steel. If you weld cold steel, the weld cools too fast, cracks, and that’s a safety hazard. Preheating the entire section (not just the spot you’re welding) brings the metal up to a consistent temperature, slows down cooling, and prevents thermal stress. A lot of guys try to use a MIG gun’s heat or even a propane torch, but that’s not enough. You need a specialized preheat torch—usually a oxy-acetylene one with a wide flame, adjustable so you can cover a 6-inch section in minutes, not hours. Pro tip: if you’re working in a cold workshop or outdoors in winter, grab a torch with a higher BTU rating. I’ve had guys tell me “my old torch works fine,” but then show me a weld that cracked a week later. Yeah, that’s the old torch talking.
Now, let’s get into the safety gear that’s not just “optional” but required. I know OSHA has a list, but I’m not here to read you regulations. Let’s talk about what actually keeps you from getting hurt. First, a proper welding helmet—not the cheap flip-up ones you can get at the hardware store for $20. Bore welding is long, hot work, and you’re looking at the arc for hours. Cheap helmets give you eye strain, and over time that leads to vision issues. Get an auto-darkening helmet with a wide view lens, adjustable shade (usually 10-14 for stick welding, 12-16 for TIG, which a lot of bore welders use), and make sure it’s comfortable enough to wear for 8-hour shifts. I’ve seen guys skip this and end up calling in sick with headaches that last for days. Not worth it.
Then, fire-resistant (FR) clothing. Not just a cotton shirt—cotton burns, melts, and sticks to your skin. FR shirts, pants, even the sleeves that go under your jacket. And don’t forget the hand protection: welding gloves that are thick, heat-resistant, but not so bulky you can’t hold your torches or clamps. I’ve had a customer come in last month with a second-degree burn on his wrist because he used a pair of old work gloves for welding. The spark went through, and he was out of work for two weeks. That’s money he lost because he tried to save $30 on gloves. Also, if you’re welding around hydraulic fluid or other flammable stuff (which you often are in bore work), grab a fire blanket and a small ABC fire extinguisher. Keep them within arm’s reach—don’t put them in the truck 10 feet away.
Wait, what about the stuff that makes your job easier, not just safer? Let’s talk about bore gauges and alignment pins. Bore welding is all about precision. If your hole is even a tenth of a millimeter off, the parts you’re putting back (like a piston or a bushing) won’t fit, and you’ll have to re-machine it. A bore gauge lets you measure the inner diameter at multiple points, so you can make sure the surface is consistent before you start welding. Alignment pins, on the other hand, hold the two parts of the bore lined up while you weld. A lot of guys use random bolts, but alignment pins are made to be a perfect fit, so you don’t get movement mid-weld. I had a guy tell me he “doesn’t need a bore gauge” and then spent 4 hours sanding the weld because the hole was oval. Yeah, that’s the “I don’t need accessories” guy we all know.
Then there’s wire brushes and grinders. You’d think that’s basic, but wait—bore welding has a lot of gunk on the surface: oil, rust, old paint, mill scale. If you don’t clean the area before welding, the weld will be porous and weak. A stiff wire brush (not a soft one for painting) gets rid of loose rust and debris, but a 4.5-inch angle grinder with a grinding disc (and a flap disc for finishing) is what you need to get a smooth, clean surface. Also, after welding, you need to grind down the excess weld so it’s flush with the bore wall. A lot of new guys use a chisel, but that leaves high spots that will wear out parts way faster. A small die grinder with a carbide burr is perfect for getting into tight spots in the bore. Pro tip: grab a bunch of extra grinding discs—they wear out fast, and there’s nothing worse than your disc breaking mid-job because you tried to grind through a thick spot.
Wait, I can’t forget about cooling systems. TIG welding, which is super common for bore work because it gives a cleaner, more controllable weld, produces a lot of heat. If your TIG torch runs too hot, it will overheat, the tungsten will get contaminated, and you’ll have inconsistent welds. A water-cooled torch and a dedicated cooling unit (not just hooking it up to a garden hose) keeps the torch at a steady temperature. I’ve had customers bring in torches that burned out in a week because they skipped the cooling unit. It’s a $200 accessory, but it saves you $800 on a new torch every few months.
Let’s talk about something that’s often overlooked: electrode holders and filler metal. Wait, filler metal is technically an accessory, right? Because you can’t weld without it. Bore work usually uses specific filler rods—E7018 for stick welding, ER70S-6 for TIG or MIG—because they have the right strength and ductility for thick steel. Don’t just grab any rod from the shelf. I’ve had guys use cheap filler rods and end up with welds that crack under pressure. Also, electrode holders: get one that’s light, has a good grip, and doesn’t get hot after 10 minutes of welding. The old heavy ones are a pain after a while, and they can lead to hand fatigue, which leads to mistakes.
Now, let’s get real. I know a lot of you are running small businesses or working out of a garage, and you don’t want to drop a ton of cash on accessories. But here’s the thing: the accessories that seem like a “waste” at first are the ones that save you time and money in the long run. Let’s do the math: that cheap back-up ring is $15, but if it melts and ruins a $2,000 cylinder, that’s a bad investment. A good welding helmet is $150, but if it saves you from headaches and vision issues, that’s worth every penny. A bore gauge is $200, but it saves you 4 hours of sanding and rework on every job.
I’m not here to sell you a bunch of useless junk. I’m here because I’ve been in this game, I’ve seen the good, the bad, and the ugly of bore welding, and I know that having the right accessories is what makes a good welder great. I supply these accessories to guys all over—from solo operators to big construction companies—and I hear every day that skipping accessories leads to headaches, rework, and lost profit.
Now, if you’re out there shopping for bore welding gear, or you need to restock your cart, don’t just go for the cheapest stuff. Look for accessories that are durable, made for bore welding specifically, not general welding. Ask questions—any reputable supplier will tell you exactly what you need, why you need it, and how it will help your jobs go smoother.
If you’re ready to put together a solid bore welding setup, or you just want to chat about what accessories would work best for your specific jobs, reach out. We can walk through what you need, no pressure, no weird upsells. Let’s make sure your next bore weld is strong, safe, and done right the first time.
Facing Head References
- Welding Handbook, Volume 4: Structural Welding, American Welding Society, 2021
- "Bore Welding Best Practices", Industrial Maintenance and Plant Operations Magazine, 2022
- OSHA Safety Standards for Welding, Cutting, and Brazing, Occupational Safety and Health Administration, 2023
- "Precision Bore Welding: Accessories and Techniques", Machinery Repair Technology Journal, 2021
- Field Guide to Industrial Welding Accessories, Welding Supply Association, 2022
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional bore welder manufacturers and suppliers in China. We warmly welcome you to buy cheap bore welder for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
