If you’re running a sheet metal fabrication shop, you’ve probably asked yourself this: is it even worth trying to connect a sheet cylindrical forming machine to an automated production line? I get it—when I first started working with these machines years ago, I thought they were just standalone workhorses. You load a sheet, punch the buttons, bend that cylinder, and you’re done. But as more customers came to me asking about streamlining their operations, I dug into this, tested a few setups, and now I can say with total confidence: yeah, it can be done. And it’s not as complicated as you might think. Sheet Cylindrical Forming Machine
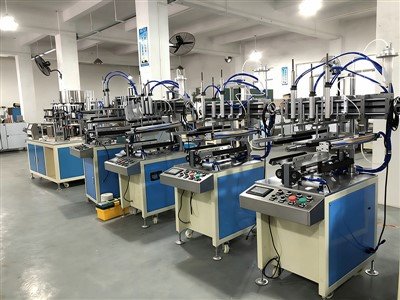
Let’s start with the basics for anyone who might not know. A sheet cylindrical forming machine (we just call them “roll formers” or “cyl formers” around the shop) bends flat metal sheets into round or tapered cylinders—think pipes, vents, solar panel housings, even some automotive exhaust parts. Traditional setups had this machine all by itself; workers would bring cut sheets from a cutting table, load them manually, adjust the machine’s dies, take the finished cylinder, and send it off to welding. That’s slow, leaves room for human error, and means you’re wasting a lot of time between steps.
Automated production lines, on the other hand, are all about continuous flow: one machine feeds into the next, no stopping, no manual handling. So the big question was: how do these two things play nice? Turns out, most modern cylindrical forming machines are already built with automation compatibility in mind. You don’t need to tear out the whole machine and start over. You just need to add a few small upgrades and link it to the rest of your line.
Let me walk you through a real example I worked on last year with a customer who makes HVAC ducting. They had a standalone cyl former that was producing 120 cylinders a day, with two workers dedicated to loading and unloading. We upgraded their machine with two things: a robotic arm pick-and-place system (we use lightweight, programmable ones that fit right on the machine’s sides) and a connection to their existing CNC cutting table. Here’s how it worked: the cutting table cuts the exact sheet size needed for each duct, the robotic arm grabs the finished cut sheet and loads it straight into the cyl former—no human touching it. The former has sensors that adjust its die gaps automatically based on the sheet’s thickness and diameter (we program that into the line’s central control system, so you don’t have to tweak the machine every time you switch parts). Once the cylinder is formed, another robotic arm takes it and feeds it to a welding machine right down the line. Suddenly, they were producing 350 cylinders a day, with zero workers stationed at the cyl former. That’s not a small win.
Now, I know what you’re thinking: “My machine’s old—can I still do this if it’s not a brand-new one?” That’s a fair question. I’ve helped customers retrofitting 10-year-old formers too. The key here is modularity. Most old cylindrical forming machines have basic control systems that you can upgrade with a PLC (programmable logic controller)—that’s the brain that connects all the machines in the line. You don’t need to replace the whole machine; just swap out the old control panel for a PLC, add a couple of input/output modules to talk to the robots and cutting table, and you’re good. I once had a customer with a 2015 cyl former that was only doing 80 cylinders a week; after retrofitting it, they hit 400 a week. It’s all about matching the upgrades to your line, not forcing a one-size-fits-all fix.
But let’s talk about the hiccups, because this isn’t just a “plug and play” deal. The biggest one we run into is sheet consistency. If your cutting table is leaving burrs on the sheet edges, or if the sheets are warped, the cyl former’s sensors will mess up. We always tell customers to make sure the upstream machines (cutting, blanking, any pre-processing steps) are up to par before connecting. If you’ve got a flimsy cutting table that spits out sheets that are off by 1/8 of an inch, the robotic arm might not grip right, or the former won’t form the cylinder evenly. It’s like building a house on a shaky foundation—you’ve got to fix that first.
Another common issue is downtime synchronization. Automated lines run on a tight schedule, so if your cyl former breaks down for even 10 minutes, it can back up the whole line. That’s why when we connect these, we make sure the former has built-in monitoring: it sends an alert to the line’s control panel if it needs a die change, or if there’s a jam, so the upstream machines slow down instead of stopping entirely. We also program in buffer stations—small areas where finished cylinders sit temporarily if the welding machine is backed up. It’s a buffer, so no machine is waiting around idling, and nothing gets stuck.
Wait, let’s not forget cost, because that’s a big one for most fabricators. I hear all the time: “I can’t afford to upgrade my machine for automation.” But here’s the thing: the return on investment is way faster than you think. For that HVAC customer I mentioned earlier, the upgrade cost about $18,000. They saved $40,000 a year in labor costs (they reallocated the two workers to other jobs) and increased revenue by $65,000 in the first 6 months. Even with a retrofitting job, which might be a bit less, you’re looking at paying off the investment in 8 to 12 months. That’s not a long time for a setup that’s going to last 15 more years.
Also, let’s get specific about the types of cylindrical forming machines that work best here. Most of the standard ones—round cylinder formers, tapered cylinder formers, even oval ones—are compatible. The trick is matching the automation components to the size of the cylinders you’re making. If you’re producing tiny cylinders (like those for medical device parts), you can use small, high-speed robots. If you’re making large industrial pipes, you’ll need heavier-duty robots and maybe a conveyor system instead of an arm. We tailor every setup to what the customer needs, so there’s no one-size-fits-all rule.
I should also mention quality control, which is a huge bonus of connecting these lines. When everything is automated, you eliminate human error in loading and forming. No more sheets being loaded crookedly, which leads to lopsided cylinders. No more misadjusted dies, which wastes material. One of my customers said their scrap rate dropped from 8% to 1.5% after connecting. That’s thousands of dollars saved in scrap metal every year, right there.
Now, if you’re thinking about taking the plunge, here’s what I recommend starting with. First, audit your current setup. What’s your output right now? Where are your bottlenecks? Is the cyl former the slow step, or is it the cutting or welding? If the former is the bottleneck, automation is a no-brainer. Second, talk to someone who knows cylindrical forming machines—someone who’s worked with retrofits and automated lines, not just a sales rep. I’ve seen customers make the mistake of buying automation parts that don’t fit their machine, wasting thousands. Third, start small. You don’t have to automate your whole line at once. Maybe start by connecting the former to the cutting table, add the robotic arm later. Test it for a month, adjust, then add more. That way, you don’t disrupt your whole operation while you’re setting it up.
Wait, let’s address a common myth I hear all the time: “Automated lines are only for big companies.” No way. I’ve worked with small shops that have 3 employees, and they’ve connected their cyl former to a basic automated line with a cheap robotic arm and a simple PLC. They’re not cranking out 10,000 parts a month, but they’re cranking out enough to make the setup worth it. It’s not about how big your shop is—it’s about how much you want to cut labor, reduce scrap, and speed up your process.
Another thing: maintenance. Automated setups do need a bit more upkeep, but it’s not hard. We give customers a simple checklist: clean the cyl former’s rollers every week, check the robotic arm’s grips monthly, calibrate the control system every quarter. It takes about 20 minutes a week, and it prevents 90% of the downtime issues. Compare that to hiring a part-time worker just to load and unload the former—this is way less work.
Let me wrap this up. The short answer is: yes, a sheet cylindrical forming machine absolutely can be connected to an automated production line. It’s not some futuristic concept; it’s something that fabricators are doing right now to save time, money, and headaches. Whether you’ve got a brand-new machine or a 10-year-old retrofitted one, as long as you’re willing to upgrade a few key parts (the control system, maybe a robotic arm or conveyor), you can integrate it seamlessly.
If you’re curious about how this would work for your shop—if you’re wondering how much it would cost, or if your machine is compatible—don’t hesitate to reach out. We’ve helped dozens of customers make the switch, and we can walk you through every step, from auditing your current setup to installing the upgrades to training your team. It’s not as scary as it sounds, and the payoff is way worth it.
Round Packaging Box Forming Machine Reference:
- Industrial Automation for Sheet Metal Fabrication, Fabricators & Manufacturers Association International, 2022
- Retrofit Guide for Forming Machines, American Machine Tool Distributors’ Association, 2021
- Efficiency Metrics in Automated Cylindrical Forming, Journal of Metalworking Manufacturing, Vol. 18, No. 3, 2023
Titagong (Dongguan) Machinery Co., Ltd.
We are one of the most reliable manufacturers and suppliers of sheet cylindrical forming machine in China. With abundant experience, we warmly welcome you to buy bulk high quality equipment in stock here and get pricelist from our factory. For price consultation, contact us.
Address: No.149, Qingyi Road, Qingxi Town, Dongguan City, Guangdong Province, China
E-mail: shuaizoe@gmali.com
WebSite: https://www.titagonggroup.com/
